Vibration sensors are suitable for collecting the working status of various equipment such as rollers, planes, and telescopic belt conveyors in the logistics and express delivery industry to achieve optimal allocation of assets within the network.
Whether you are seeking customized solutions or general-purpose products, we are committed to providing you with high-quality, cost-effective products, and services. Feel free to send us your inquiries and orders, and we will respond promptly with detailed product quotations.
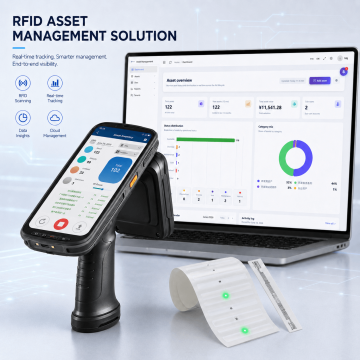 RFID Asset Management Kit
 IP67-protected Integrated RFID Reader Writer RFly-I165 for Supply Chain
 Long-range Distance UHF RFID Reader RFly-I195 for Inventory Management
 Small UHF RFID Tag Reader RFly-I300 for Cars
 Two-channel Compact Fixed RFID Reader RFly-F210 for Warehousing
 Four Channels Fixed UHF RFID Reader RFly-R6 for Supply Chain
 8-channel UHF RFID Tag Reader RFLY-MR8 for File Cabinet Identification-1
 USB Compact Desktop RFID Scanner GRU-D100 for Card Management
 Bluetooth Portable RFID Reader and Writer GRU-HBT100 for Inventory Management
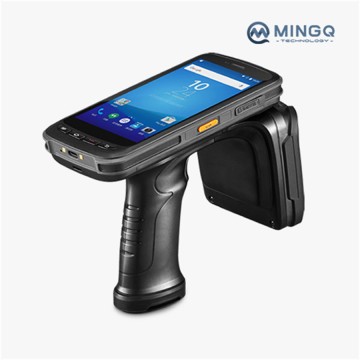 Industrial Grade Handheld UHF RFID Reader GRU-HC520 Suitable for Logistics
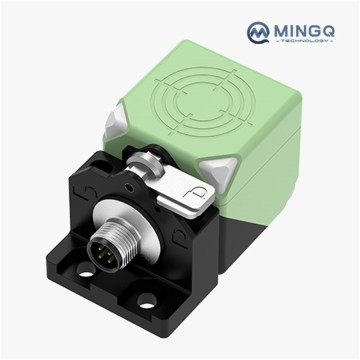 Rotary HF RFID Tag Reader GRH-I40 Suitable for Assembly Lines
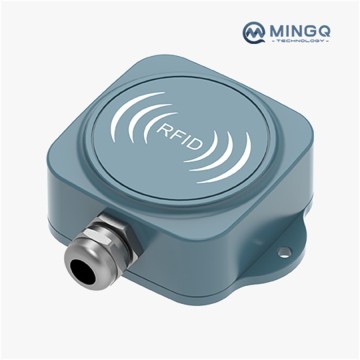 Industrial-grade High-frequency Integrated Reader GRH-I65 Suitable for Asset Tracking
 With ESD Protection HF RFID Reader GRH-I68 Suitable for Progress Tracking
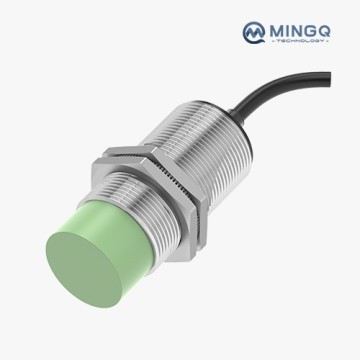 Proximity HF RFID Reader GRH-M30 Suitable for Manufacturing Workshops
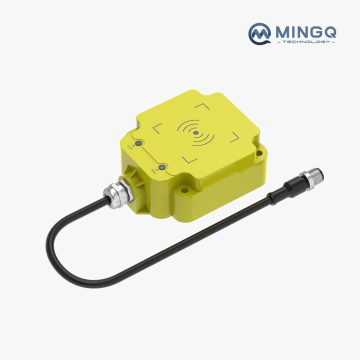 High Frequency Medium Distance Reader GRH-I90 Suitable for Logistics Production Line
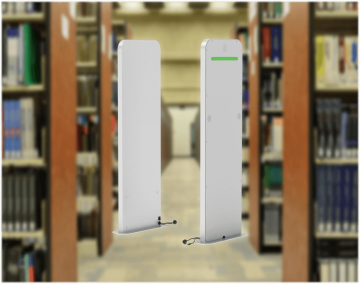 UHF RFID Portals and Tunnel Machine RFly-AM3000 for Access Control
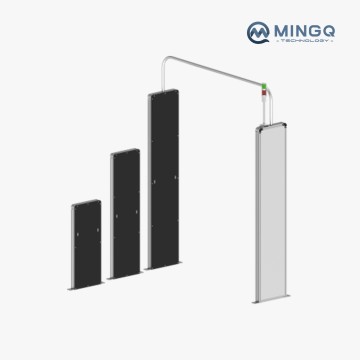 Narrow RFID Portals Series TD-P20040-SS for Single Tag Entry and Exit Identification Scenario
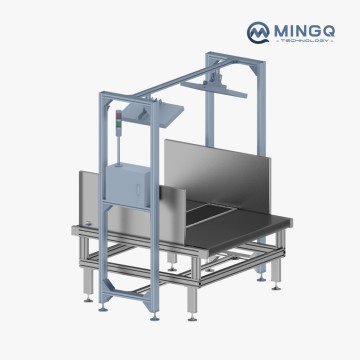 RFID Transmission Line Simple Identification Tunnel Machine (TD-T3050)
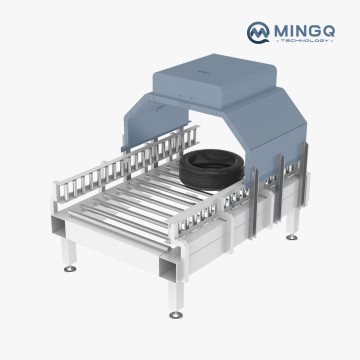 Vision and RFID Tunnel Machine TD-T7692-RV for Logistics Sorting
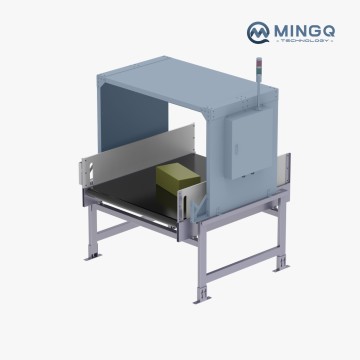 RFID Transmission Line Identification Tunnel Machine TD-T10090
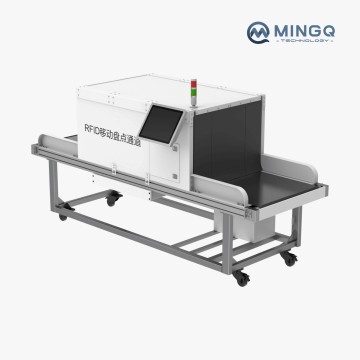 RFID Mobile Inventory Tunnel Machine TD-T65150 for Conveyor Belts
 RFID Tags for Container Turnover Management
 RFID Tags for Equipment O&M Management
 RFID Tags for Manufacturing Management
 RFID Tags for Tool Management
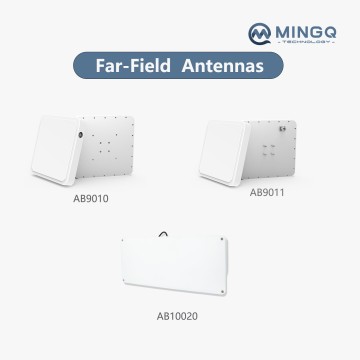 High-Performance Far-Field Antennas for Broad Coverage.
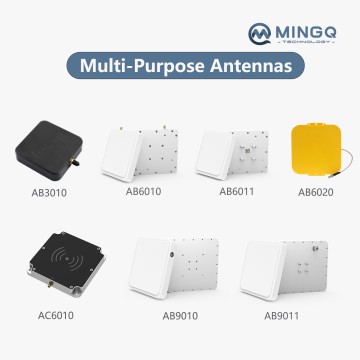 Multi-Purpose Antennas: Flexibility for Diverse Applications
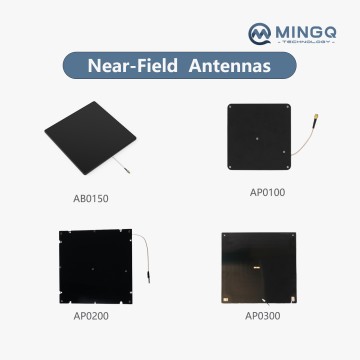 Near-Field Antennas for Short-Distance Tag Detection.
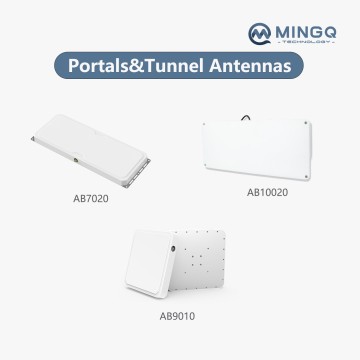 Portals & Tunnel Antennas for Integrated RFID Series
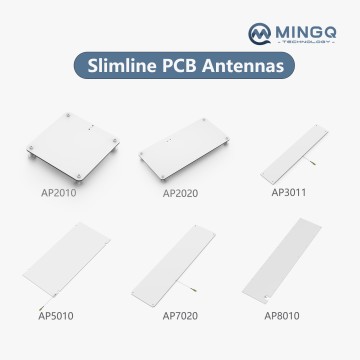 Slimline PCB Antennas for Warehousing and Logistics
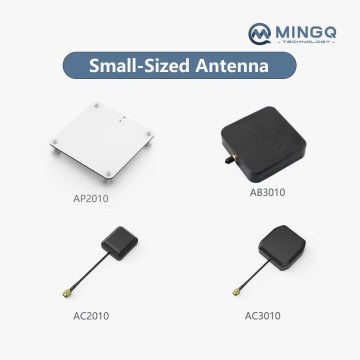 Miniaturized and Thin Antennas can Provide Good Performance in a Smaller Size.
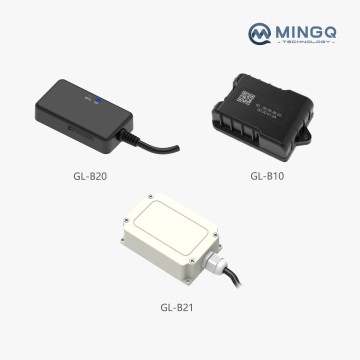 GPS Tracker for Vehicles, Car, Kids, Assets.
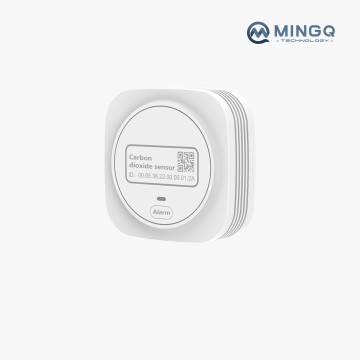 CO2 Sensors Detect CO2 Gas through Alarms, Suitable for Offices, Planting Tents.
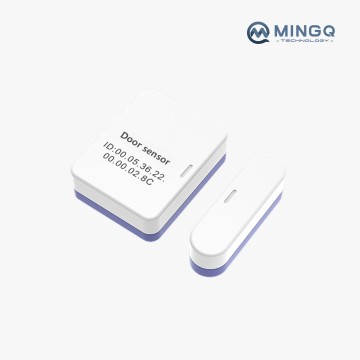 Door Sensor, Detect Open and Closed Doors or Windows, Sends Alerts, Triggers Siren.
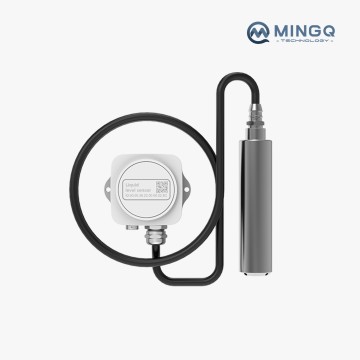 Wireless Level Sensor Equipped with a 5-Meter Detection Line, Suitable for Water Tanks
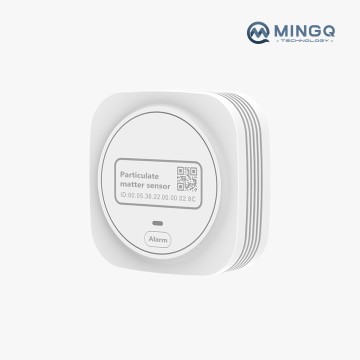 Real Time Monitoring of Air Quality Using PM2.5/PM10 Sensors.
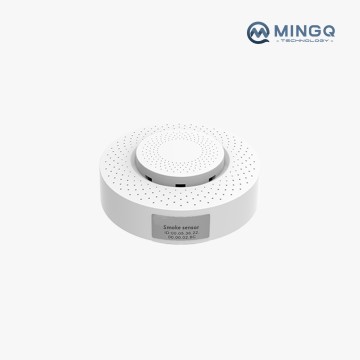 Smoke Sensor, Fire Alarm Smoke Detector with Test Button and Low Battery Reminder.
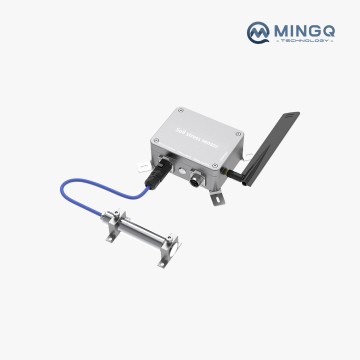 Soil Stress Sensor,Bridge and Tunnel Monitors.
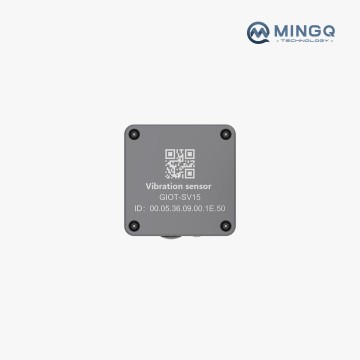 Vibration Sensor Monitors Equipment, Like Conveyors and Motors, for Operational Status.
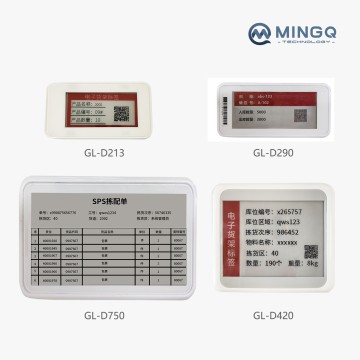 E -Paper Display
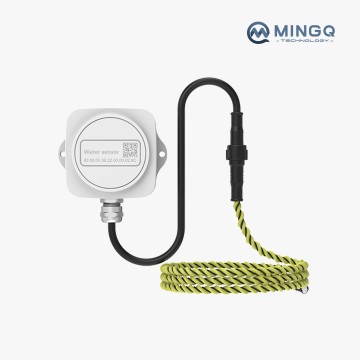 Smart Water Sensor Alarms, 1.2 M Detection Line.
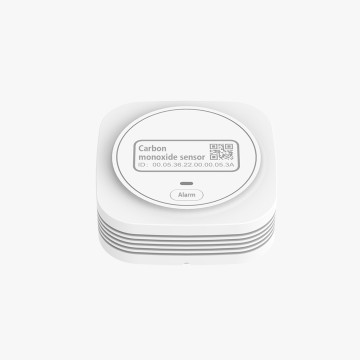 CO Sensor for Basements Home Office House Bedroom Living Room Car, Light Plug and Play.
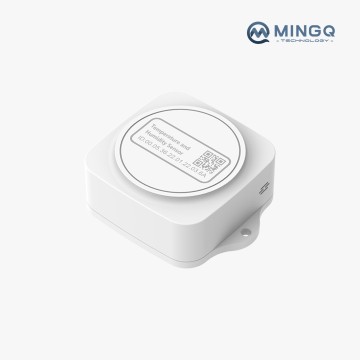 Temperature and Humidity Sensor
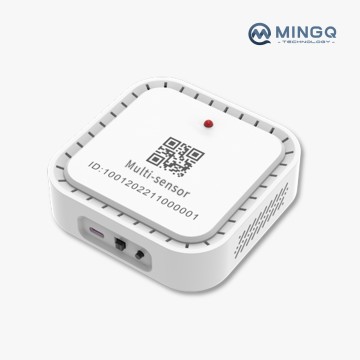 Multi-sensor GD-ME
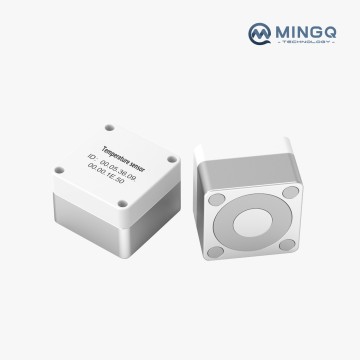 Temperature Sensors Monitor the Surface Temperature of Various Heating Equipment.-1
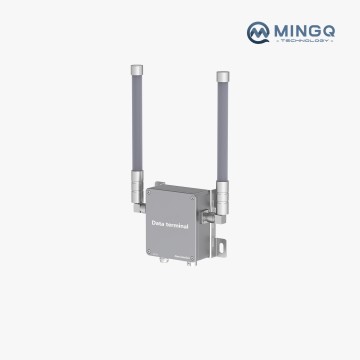 Signal Enhancement Terminal, Long Range Coverage.
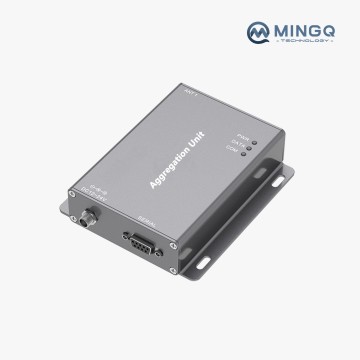 Multi-Protocol Communication Gateway, App Remote Control.
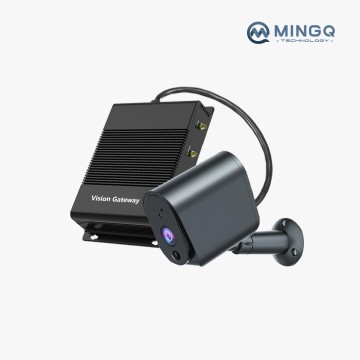 Edge Vision Gateway can Access Various Mainstream Cameras, Suitable for Office, Factory.
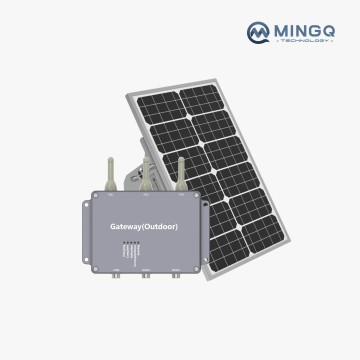 GBS-3550 Outdoor Sensor Gateway,LoRa, 2/3/4G Communication.
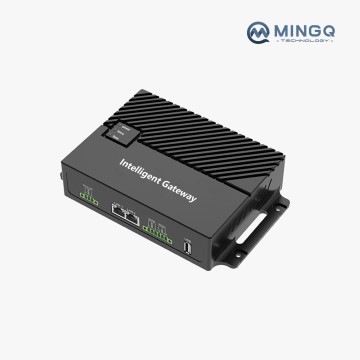 Smart WiFi Gateway, Realize Remote Control.
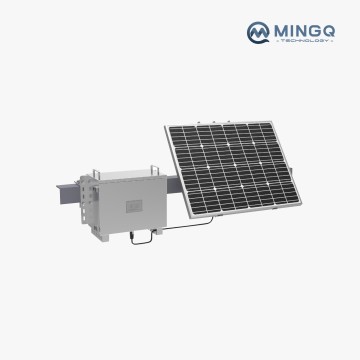 Ultra-Low-Power Solar-Powered Intelligent Gateway (Outdoor)
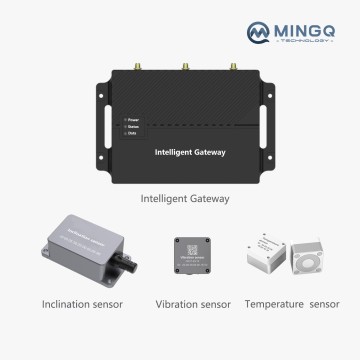 A Kits for Equipment Condition Detection
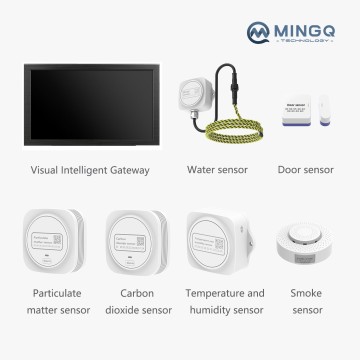 A Kits for Office Computer Room Environment Monitoring
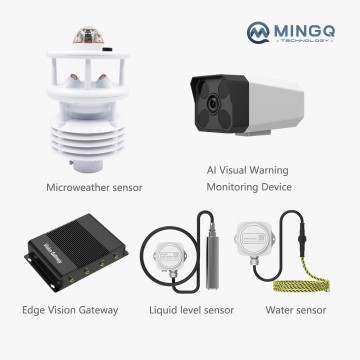 A Kits for Reservoir Environmental Monitoring
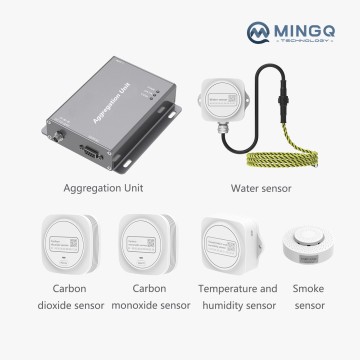 A Kits for Storage Space Environment Monitoring
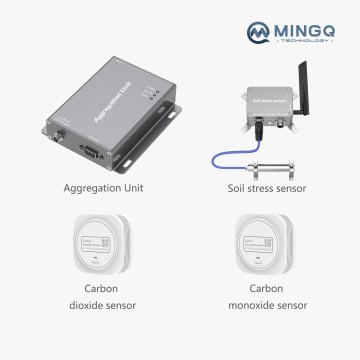 A Kits for Stress Detection of Underground Tunnel
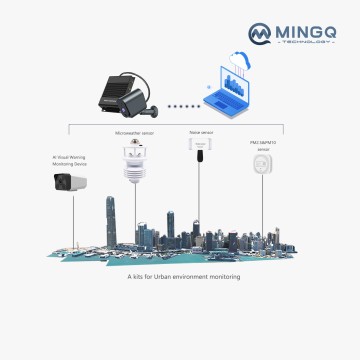 A Kits for Urban Environment Monitoring
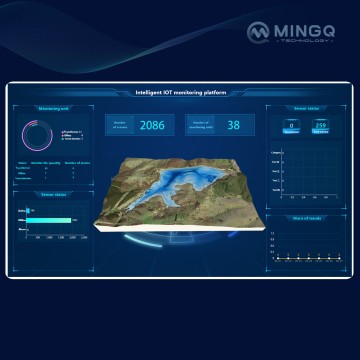 Intelligent IoT Monitoring Platform
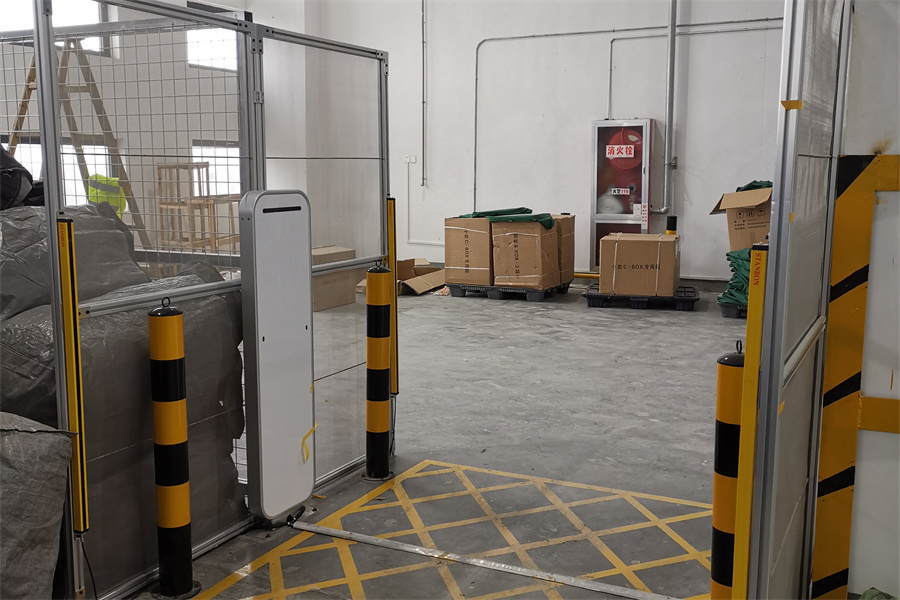 Global 3PL Streamlines High-End Fashion Inventory with MingQ RFID Tunnel Solution
 Leading E‑Commerce Platform Accelerates Flash-Sale Fulfillment and Boosts Warehouse Productivity with MingQ RFID Sorting Wall Solution
 Global Automaker Elevates Component Kitting Accuracy with MingQ RFID Shelf‑Level Management Solution
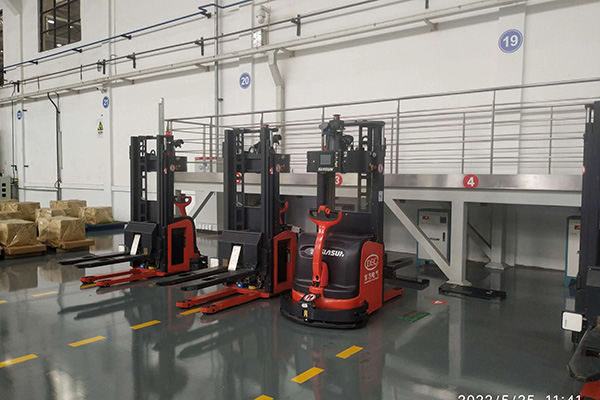 Asia’s Largest Logistics Provider Enhances Warehouse Intelligence with RFID Pallet & Container Management Solution
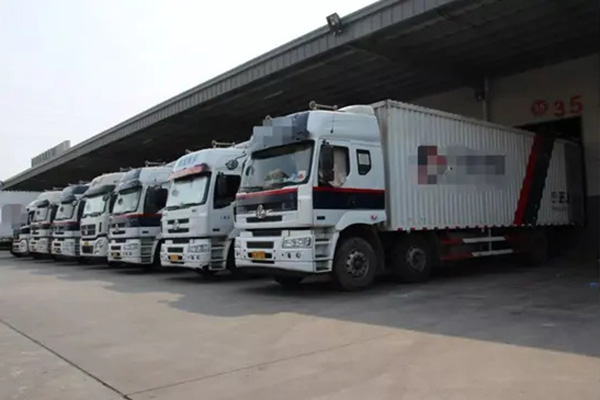 RFID Application in Platform Vehicle Management
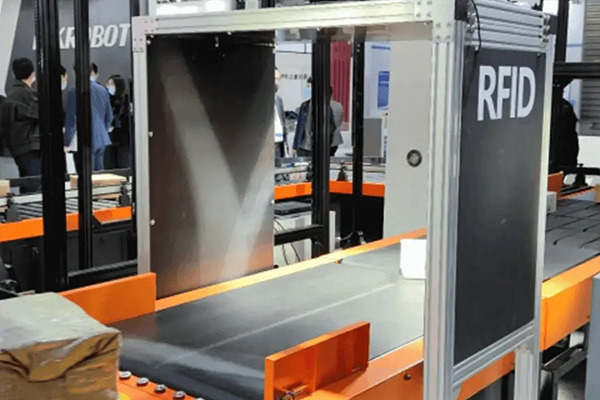 RFID Application in Logistics Sorting
 RFID Application in Supply Chain Management
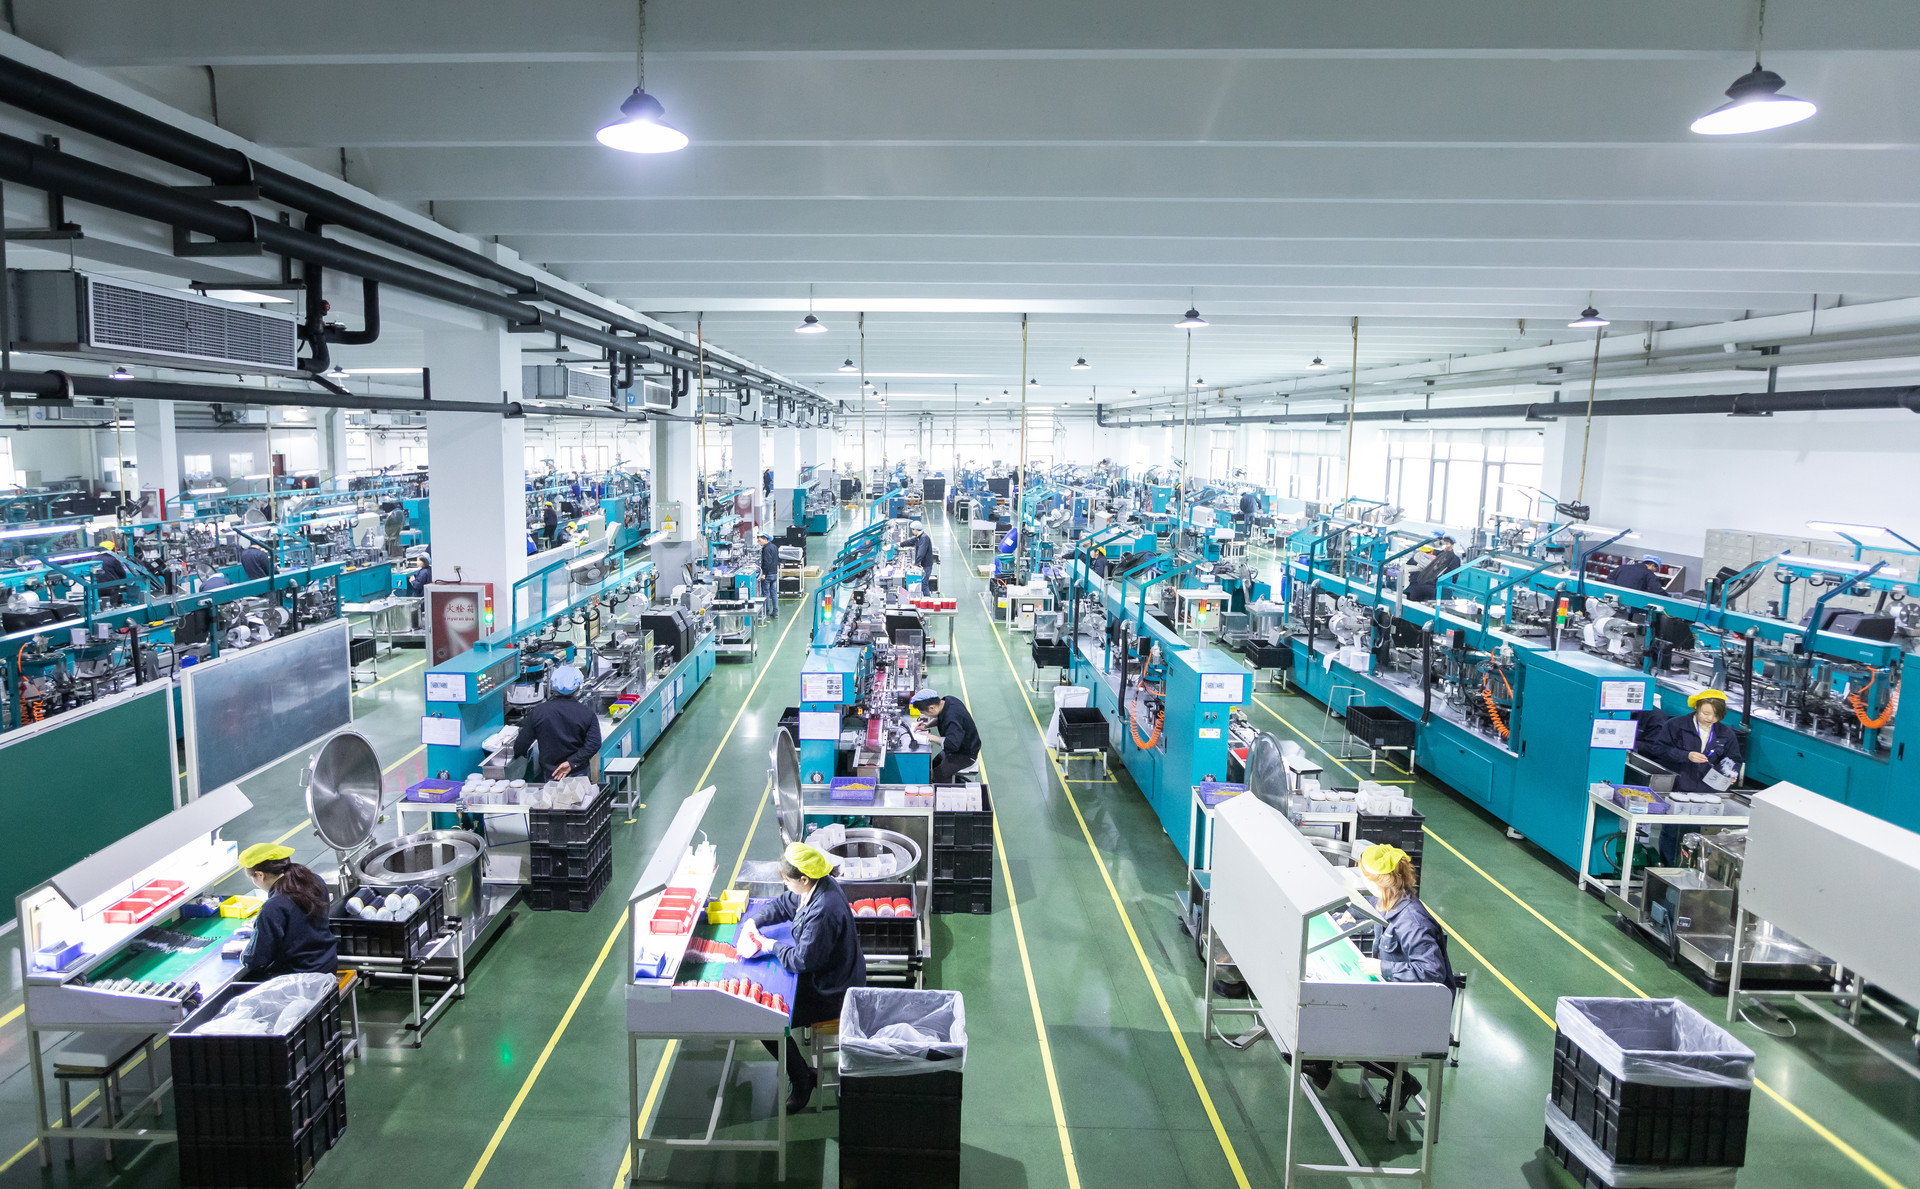 RFID Application for Workshop/Warehouse Tracking
 TP‑Link Enhances Warehouse Inbound/Outbound Efficiency with MingQ RFID Dock‑Door Solution
 RFID technology empowers port containers: a new direction for future logistics
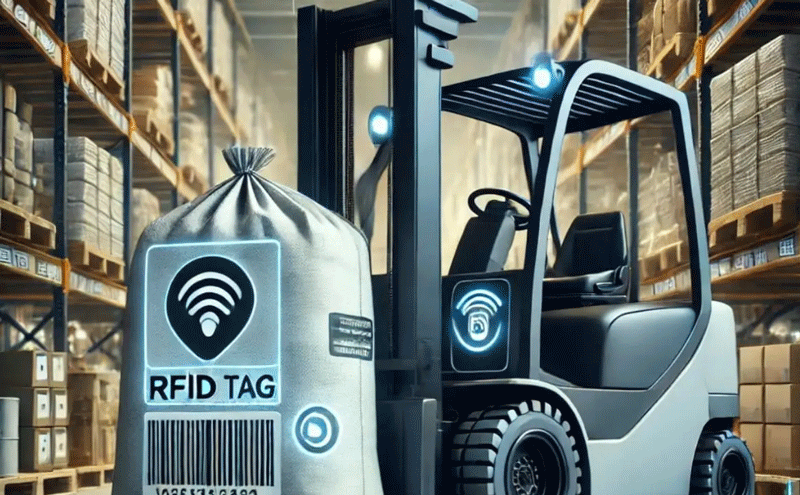 RFID technology in forklift tracking and container bag identification
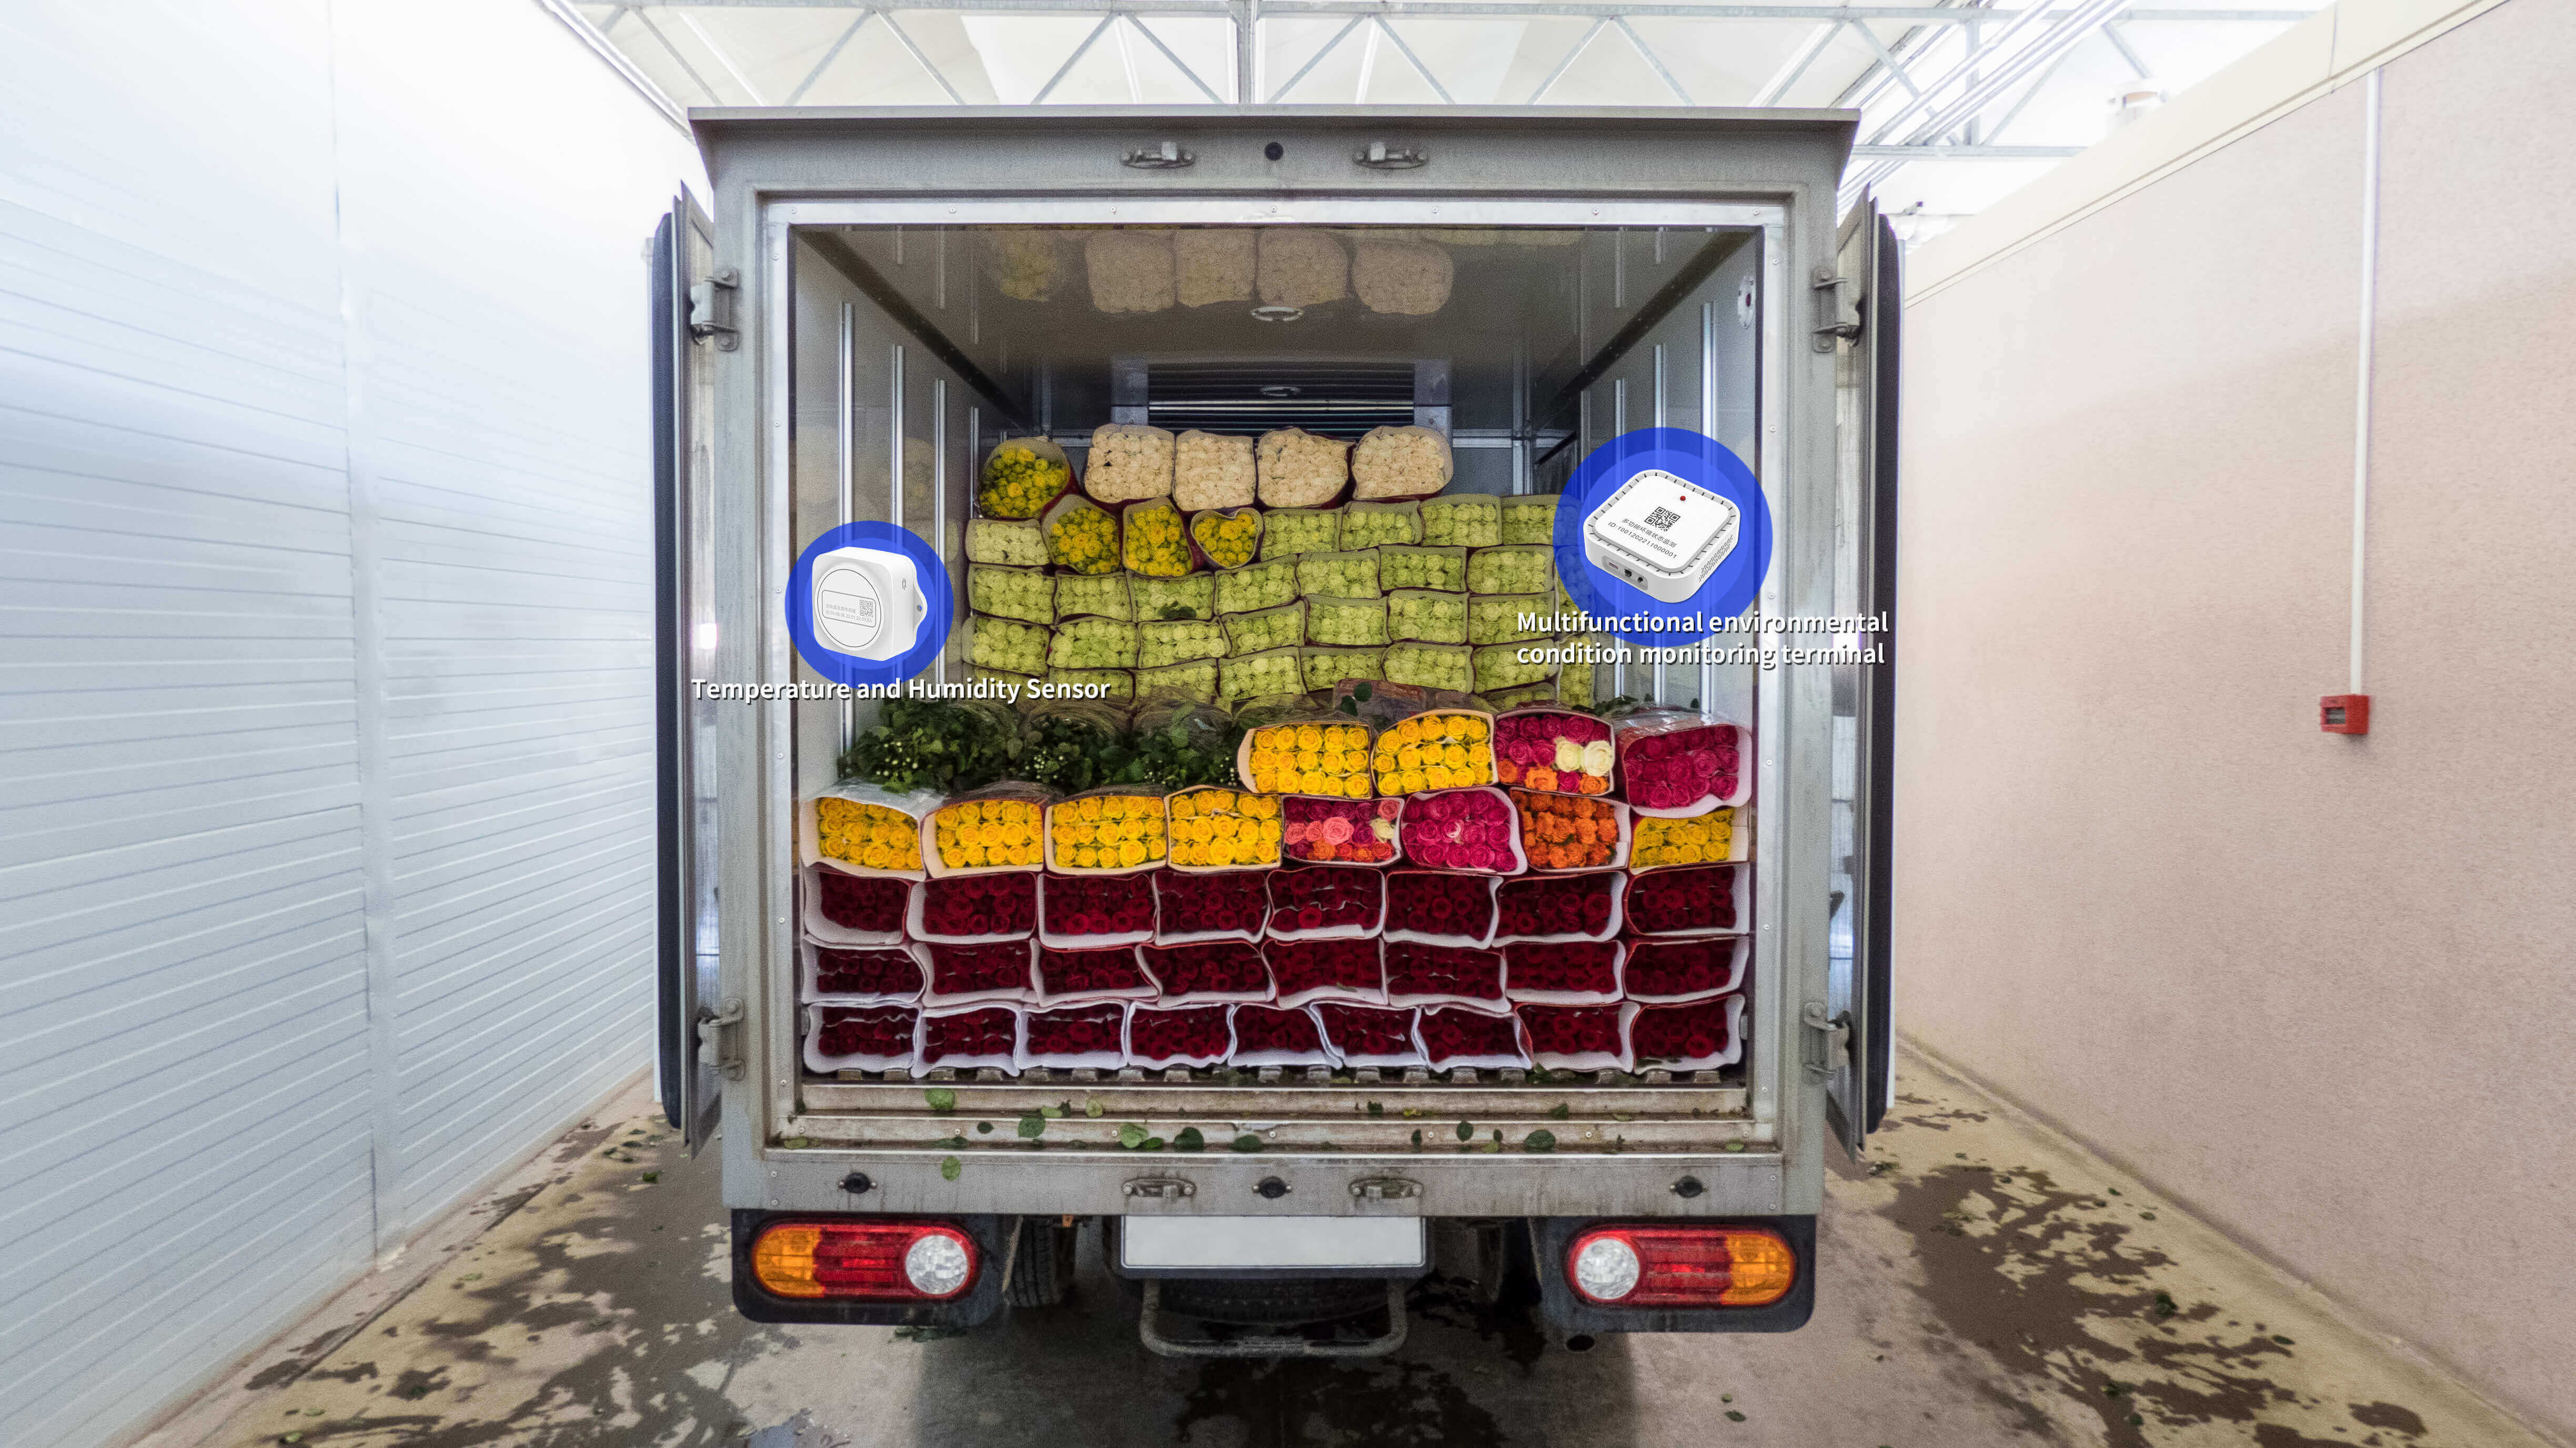 Real-Time Data, Secure Transportation: The Future Trends of Cold Chain Logistics
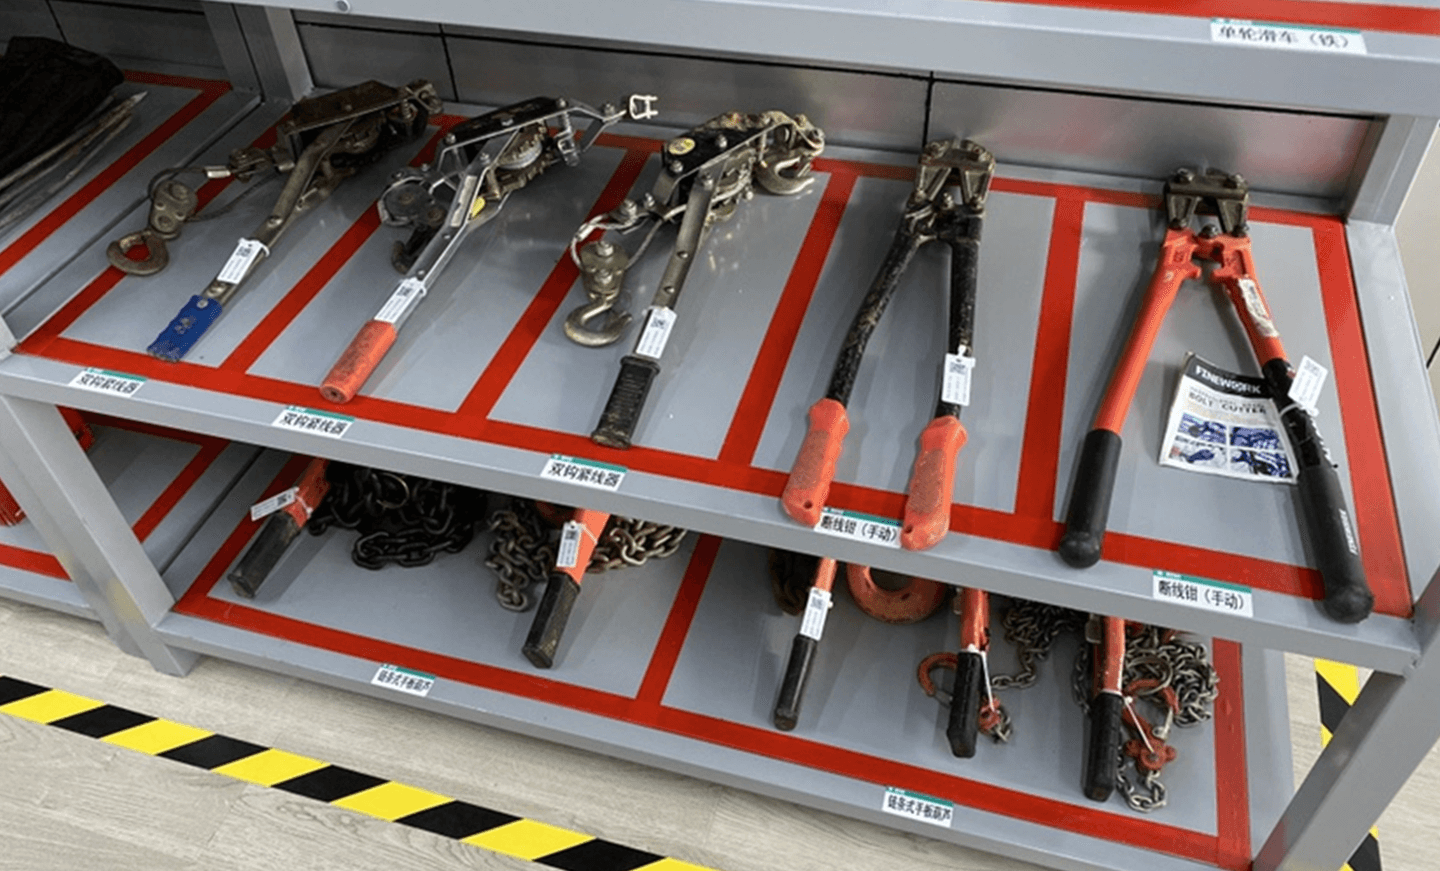 RFID Tool Management
 RFID Application in Battery Factory Production
 RFID Application in Production Line Rubber Box Management
 RFID Application in Mold Management on Production Lines
 RFID Application in Fiber Optic Cable Manufacturing
 Smart Manufacturing
 The medical industry uses RFID technology to make drug tracking more accurate
 RFID technology helps beverage production and build an efficient supply chain
 RFID technology helps car seat production lines: intelligent management improves efficiency and quality
 RFID technology in the production of electronic appliances monitoring and tracing application
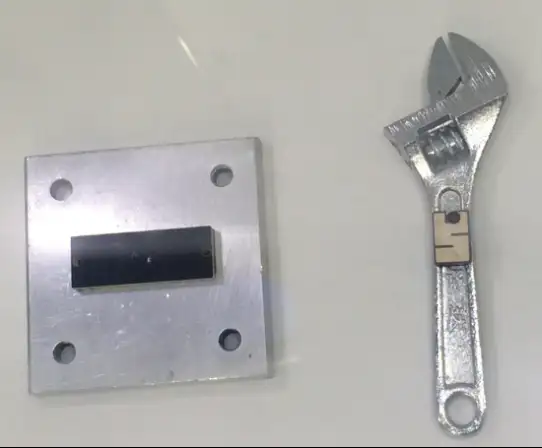 Use RFID technology to improve appliance management efficiency and security
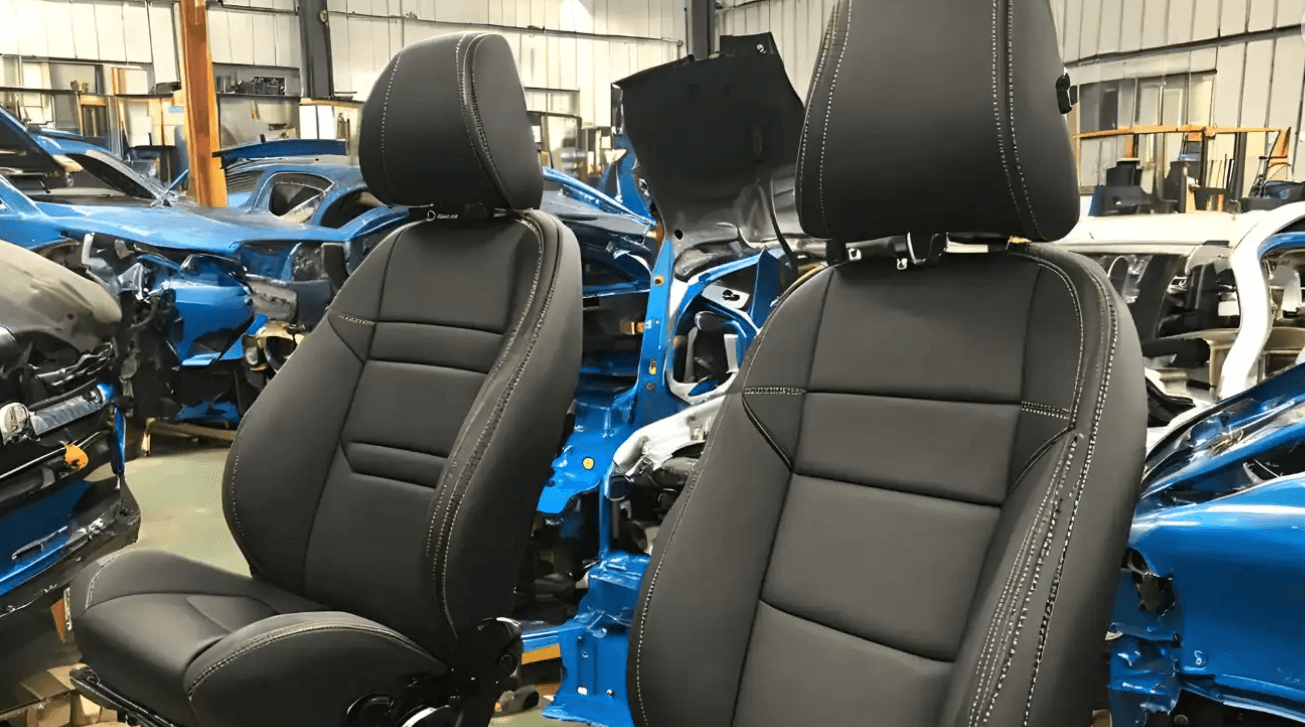 RFID technology helps precise installation of headrests